
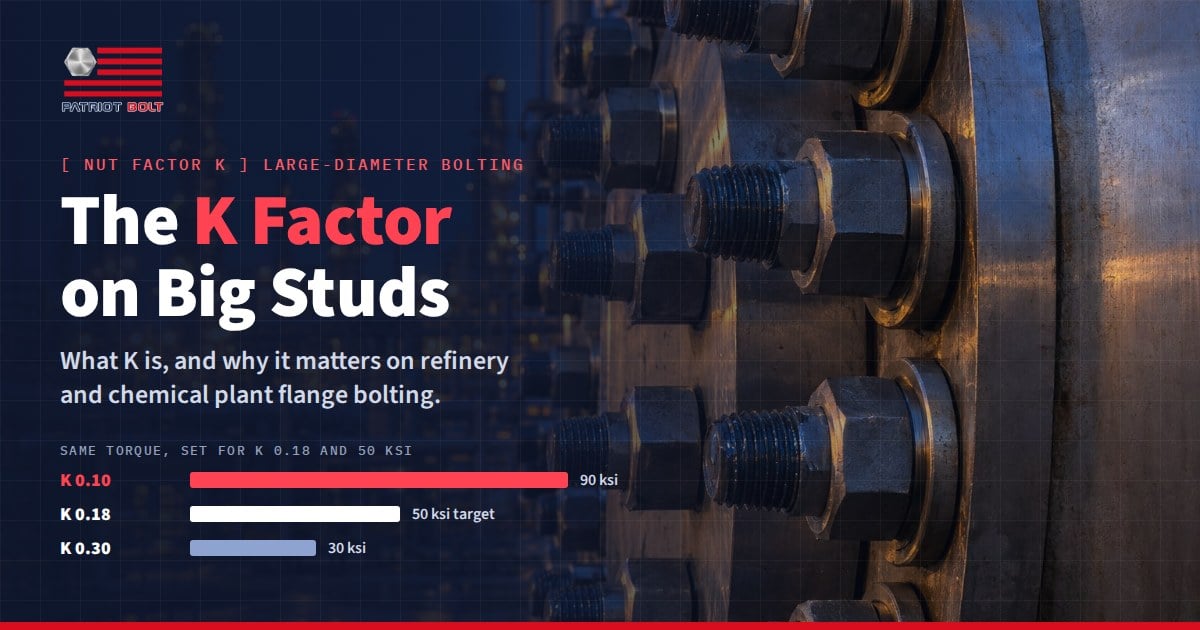
Every torque value on a flange bolting procedure hides one number: the nut factor, K. It converts the torque on the wrench into load in the stud. On a 3/4 in. stud a wrong K costs a few ft-lb. On the 2 in. to 4 in. studs on refinery heat exchangers, reactors and high-pressure piping, the same error can mean thousands of ft-lb, a yielded stud or a joint that leaks at start-up.
What the K factor is
The short-form torque equation used in most flange bolting procedures, including ASME PCC-1, is:
T = K × D × F / 12
- T = target torque, ft-lb
- K = nut factor (dimensionless)
- D = nominal stud diameter, in.
- F = target bolt load, lbf (bolt stress × area)
K is often called the nut factor or torque coefficient. It is not the friction coefficient of the lubricant, although the two are related: K is roughly the friction coefficient plus about 0.04. K is an experimental number. It is measured by tightening real studs and nuts with a real lubricant and recording torque against load. It applies only to the combination that was tested.
Only a small part of the torque on the wrench actually stretches the stud. Most of it is lost to friction under the nut face and in the threads.
Figure 1
Where the tightening torque goes
The long form: what is inside K
PCC-1 Appendix K also gives a more detailed formula, based on the VDI 2230 approach, that splits the torque into three parts:
T = F × (0.16 p + 0.58 μt d2 + μn De / 2)
- p = thread pitch (1/8 in. for 8UN). This term stretches the stud.
- μt, d2 = thread friction coefficient and pitch diameter
- μn, De = nut-face friction coefficient and effective bearing diameter of the nut
Divide by F × D and you get K. Working it through for standard heavy hex nuts shows something important for large-diameter bolting. Flange studs 1 in. and larger use 8 threads per inch whatever the diameter. So the pitch term, the only part that does useful work, shrinks as the stud gets bigger: about 0.020 of K at 1 in., but only 0.0067 at 3 in.
Figure 2
Calculated parts of K by stud diameter
Two practical points follow. First, at the same friction, geometry alone makes K slightly lower on big studs. Second, on a 3 in. stud about 95% of the torque goes into friction. Small changes in lubricant, coating, nut face condition or temperature therefore move the bolt load almost one-for-one.
Why large-diameter bolting magnifies K errors
Bolt load rises with the stud’s area (diameter squared), and torque is load times diameter. So torque grows roughly with the cube of diameter. The table shows the torque needed for 50 ksi on the root area. We calculated root area from the ASME B1.1 minor diameter, d − 1.22687p.
| Stud | Root area, in² | Load at 50 ksi, kip | K 0.12, ft-lb | K 0.16, ft-lb | K 0.20, ft-lb |
|---|---|---|---|---|---|
| 1-8 | 0.563 | 28 | 280 | 380 | 470 |
| 1-1/2-8UN | 1.424 | 71 | 1,070 | 1,420 | 1,780 |
| 2-8UN | 2.678 | 134 | 2,680 | 3,570 | 4,460 |
| 2-1/2-8UN | 4.325 | 216 | 5,410 | 7,210 | 9,010 |
| 3-8UN | 6.364 | 318 | 9,550 | 12,730 | 15,910 |
| 4-8UN | 11.621 | 581 | 23,240 | 30,990 | 38,740 |
Values are for illustration. Your target stress should come from the joint design, for example the gasket stress method in PCC-1 Appendix O. Whatever method you use, keep the bolt load and the torque on the same area basis. Appendix O works on root area, while the Appendix K-2 formula uses tensile stress area by default. Our article on tensile stress area vs root area explains the difference.
Figure 3
Target torque grows with the cube of diameter
Size also changes how the joint is tightened:
- Hydraulic torque wrenches take over once torque passes what can be done by hand, typically above about 500 ft-lb, which is reached at about 1 in. PCC-1 notes that nut factor variation with hydraulic torque tools is often 20% or more. Use a tool that will run within 20–80% of its range. Air impact guns are not a controlled tightening method. See Powered Torque Tools.
- Hydraulic tensioning pulls the stud directly and does not depend on K at all. PCC-1 describes it as generally used on studs 2 in. and larger. It needs at least one diameter of extra stud length above the nut, and it is less accurate on short studs with a length-to-diameter ratio under 5. Our stud bolt length calculator and bolt tensioning pressure calculator help with both.
- Breakout torque at the next turnaround is often higher than makeup torque, especially after high-temperature service. Choose a lubricant rated for the temperature and plan tools for disassembly as well as assembly.
Same torque, different K
The real risk is a mismatch between the K assumed in the torque table and the K the joint actually has. If a torque is calculated for K 0.18 and a 50 ksi target, here is what the stud sees when the actual K is different:
Figure 4
Bolt stress from one torque value when the actual K differs
A K of 0.10 on a torque set for 0.18 delivers about 90 ksi. That is well past the 80 ksi minimum yield of B7M and L7M sour-service studs, and close to the 95 ksi minimum yield of B7 over 2-1/2 in. At the other end, a dry or rusty stud at K 0.30 reaches only about 30 ksi, which may not seat the gasket. PCC-1 Appendix N puts typical bolt load scatter from torque on new, untested fasteners at about ±30%. Well-lubricated bolting can be held mostly within ±15%, and often within ±10%.
Refinery and chemical plant factors that change K
Refinery and chemical plant joints combine large studs, alloy and stainless materials, coatings, wide temperature swings and reused hardware. Each one moves K:
| Factor | Effect on K | What to do |
|---|---|---|
| Lubricant type | Sets the baseline | Use the K published for the lubricant you apply. Patriot Moly-B has a specified K of 0.100, and Nickel 328 runs from 0.172 down to 0.120 as bolt load rises. Never swap lubricants without recalculating torque. |
| Stainless (B8, B8M) and nickel alloys | Higher, about 30% vs B7 | Stainless and nickel alloys gall easily and run a higher K with the same lubricant. Lubricate the threads and nut faces generously and do not reuse torque values set for B7. |
| B7M, L7M (sour service) | Similar to B7 | K is similar, but the minimum yield is 80 ksi instead of 105 ksi, so a low actual K can push the stud past yield. Leave margin. |
| PTFE (fluoropolymer) coating | Lower, about 0.10–0.13 | Use the coater’s K. Torque set for uncoated, lubricated studs can overload coated ones. See Coatings for Bolting. |
| Hot-dip galvanized | Higher, about 0.18–0.25 dry | Thick and variable. Lubricate, and keep coating off the nut bearing face (PCC-1 flags more than 0.005 in.). |
| Washers and nut faces | Rough or soft faces raise it | Use through-hardened flange washers, which give a smooth, consistent bearing surface. Remove paint, scale and burrs from spot faces. |
| Ambient temperature | Can shift by 50% | One lubricant measured K 0.155 at 32 °F and 0.105 at 100 °F. A winter turnaround and a Gulf Coast summer job may need different torques. |
| Reused or rusty studs | Higher and less consistent | Clean and inspect threads, chase nuts by hand, or replace. See the Bolt and Nut Reuse Guide. |
| Hot retorque | Changes with temperature | Start-up retorque is usually done at 300–450 °F with K adjusted for temperature. After days at temperature, torque is a poor measure of load. |
Lubricant choice in process plants is also about compatibility, not just K and temperature. Copper-bearing anti-seize is usually avoided in ammonia, acetylene and vinyl monomer service. Stainless and nickel-alloy bolting usually calls for nickel or metal-free grades with low halogen and low sulfur content. Check the plant’s approved lubricant list and the process fluid before you choose. A lubricant’s maximum temperature rating tells you nothing about its K. See Thread Lubricant Temperature Ratings Explained and How to Lubricate Flange Bolting.
Getting K right on large studs
- Use the K for the actual combination: stud material, nut, coating, washer and lubricant. If any one changes, recalculate the torque.
- Lubricate every working surface: the threads under the nut and the nut face, on both ends. PCC-1 calls for this whatever the tightening method.
- Use through-hardened washers and clean, flat spot faces so the nut-face friction stays consistent.
- Keep the area basis consistent between the target stress and the torque table, either root area or tensile stress area.
- Size the tool to the torque, and consider tensioning for studs 2 in. and larger, allowing for the extra stud length.
- Verify on critical joints. Measure stud elongation with ultrasonic or mechanical methods to confirm the load and back-calculate the real K for your materials. Our bolt elongation calculator gives the target stretch.
- Adjust for temperature on hot retorque passes. See Relaxation and Retorque Passes.
For the short PCC-1 summary and a printable sheet, see the Nut Factor (K) Guide. To turn a gasket stress into a torque value, use our Gasket Stress Target Torque Calculator.
Large-diameter bolting for a turnaround? Patriot Bolt manufactures stud bolts and heavy hex nuts in B7, B7M, L7M, B16, B8M and nickel alloys, with coatings, through-hardened washers and thread lubricants on the same order, with mill test reports. Send us your bolting list. Request a quote or call (281) 581-0176.


